Routine Production Using Coffee Beans and Ground-Coffee Packing
Plan routine production using coffee beans and ground-coffee packing around representative products, packs and packaging materials, line connections, operating limits, acceptance checks and next steps.
In brief
For routine production using coffee beans and ground-coffee packing, start with representative products, packs and packaging materials and your full operating sequence, then check the credible product, pack, cleaning and line-rate extremes before committing to a final layout.
Plan coffee packing machines around your product, pack range, target output, cleaning needs and finished-pack checks. Discuss a practical line concept with Lancing using representative samples.
On the production floor
Plan for the conditions your team handles every day — Coffee Packing Machines
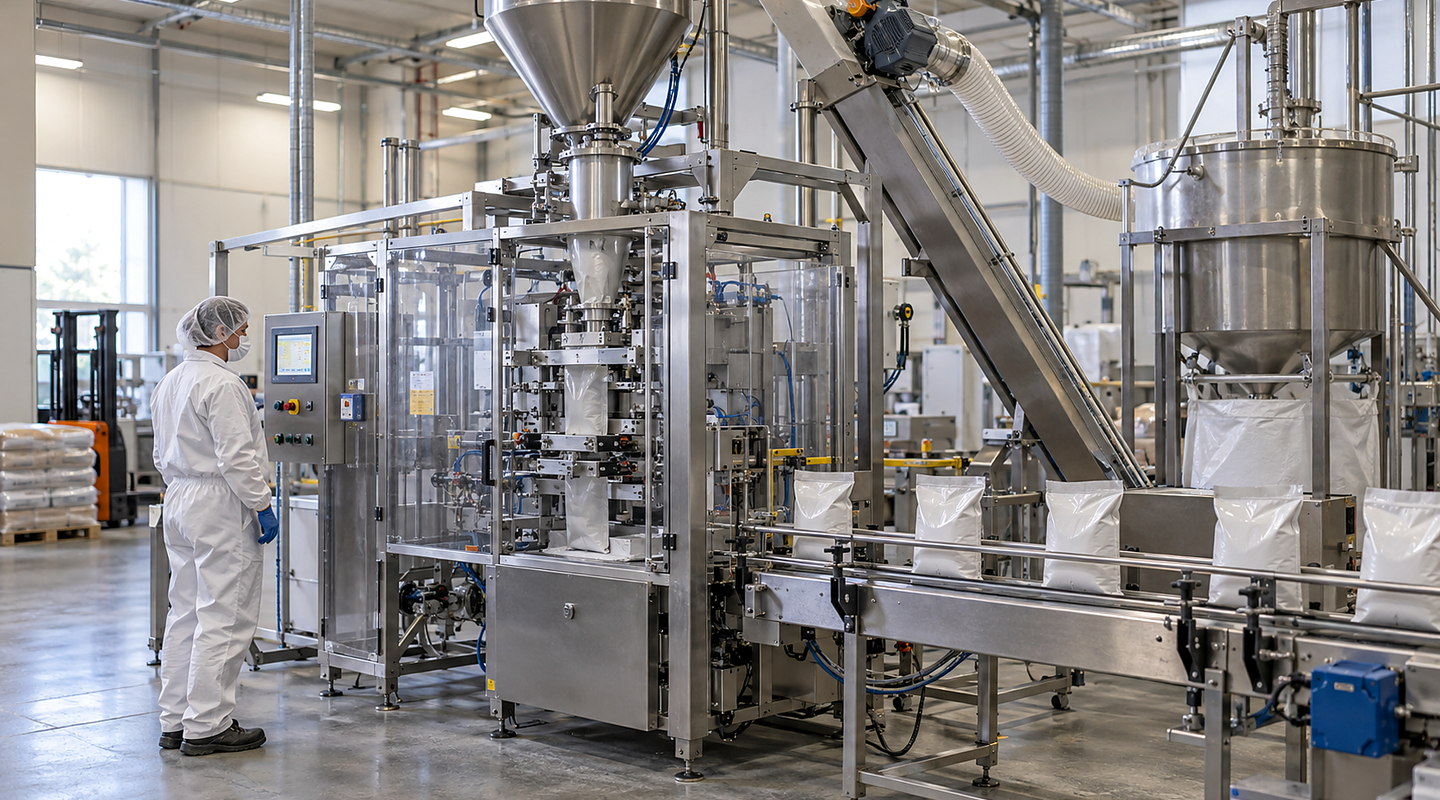
Plan coffee packing machines around your product, pack range, target output, cleaning needs and finished-pack checks. Discuss a practical line concept with Lancing using representative samples. For routine production using coffee beans and ground-coffee packing, the deciding details include coffee beans & ground-coffee packing product behaviour, target dose, count or pack weight and finished-pack checks and reject handling.
Say whether you need to pack whole beans, ground coffee or both, and describe the product condition and known variation between batches. Agree which representative samples and difficult cases should be included in a trial.
Question 2
Container, Bag or Pack Range
List each container or bag format, its dimensions, material, closure and target weight. Identify the smallest and largest packs and agree examples of the actual packaging for a trial.
Question 3
Target Dose, Count or Pack Weight
Give the target dose, count or pack weight for each format, the acceptable range and the way finished packs will be checked. Define how out-of-limit packs should be identified and handled.
Question 4
Required Output and Production Pattern
State the sustained output you need for each format and how production is scheduled. Include product replenishment, pack presentation, planned stops, checks and cleaning when comparing the complete operating cycle.
Question 5
Cleaning, Access and Changeover Method
Describe how the product-contact area and surrounding equipment need to be accessed, cleaned and changed over. Include who carries out the work and how the setup is checked before production restarts.
Question 6
Finished-Pack Checks and Reject Handling
Define the finished-pack checks, acceptance limits and result record needed for your coffee and packaging. Agree what happens to rejected packs and how the line returns to normal production after a fault.
Your operating cycle
Plan for more than automatic running
Include replenishment, normal production, planned change, short stops, fault recovery, cleaning and maintenance for routine production using coffee beans and ground-coffee packing. A fast automatic step can still leave your team with a slow or awkward overall process.
Normal production and variant changes
Replenishment and material presentation
Operator access and safe interventions
Cleaning, maintenance and recovery
Prove the result
Test routine production using coffee beans and ground-coffee packing against representative products, packs and difficult production conditions
Normal production
Run the agreed product or part mix for routine production using coffee beans and ground-coffee packing at your intended operating pattern.
Difficult conditions
Include credible extremes for coffee beans & ground-coffee packing product behaviour and container, bag or pack range.
Fault and recovery
Show how the proposed solution detects a problem affecting routine production using coffee beans and ground-coffee packing, responds safely, informs your team and restarts under control.
Important limits
Be clear about what the trial has shown
Food-contact, hygiene and allergen controls must be validated for the actual product and site.
The selected method must be trialled with representative product and packaging.
Supplier tolerances and product-condition changes can alter handling or fill behaviour.